logo
Supal (Changzhou) Precision Tools Co.,Ltd
O nas
Twój profesjonalny i niezawodny partner.
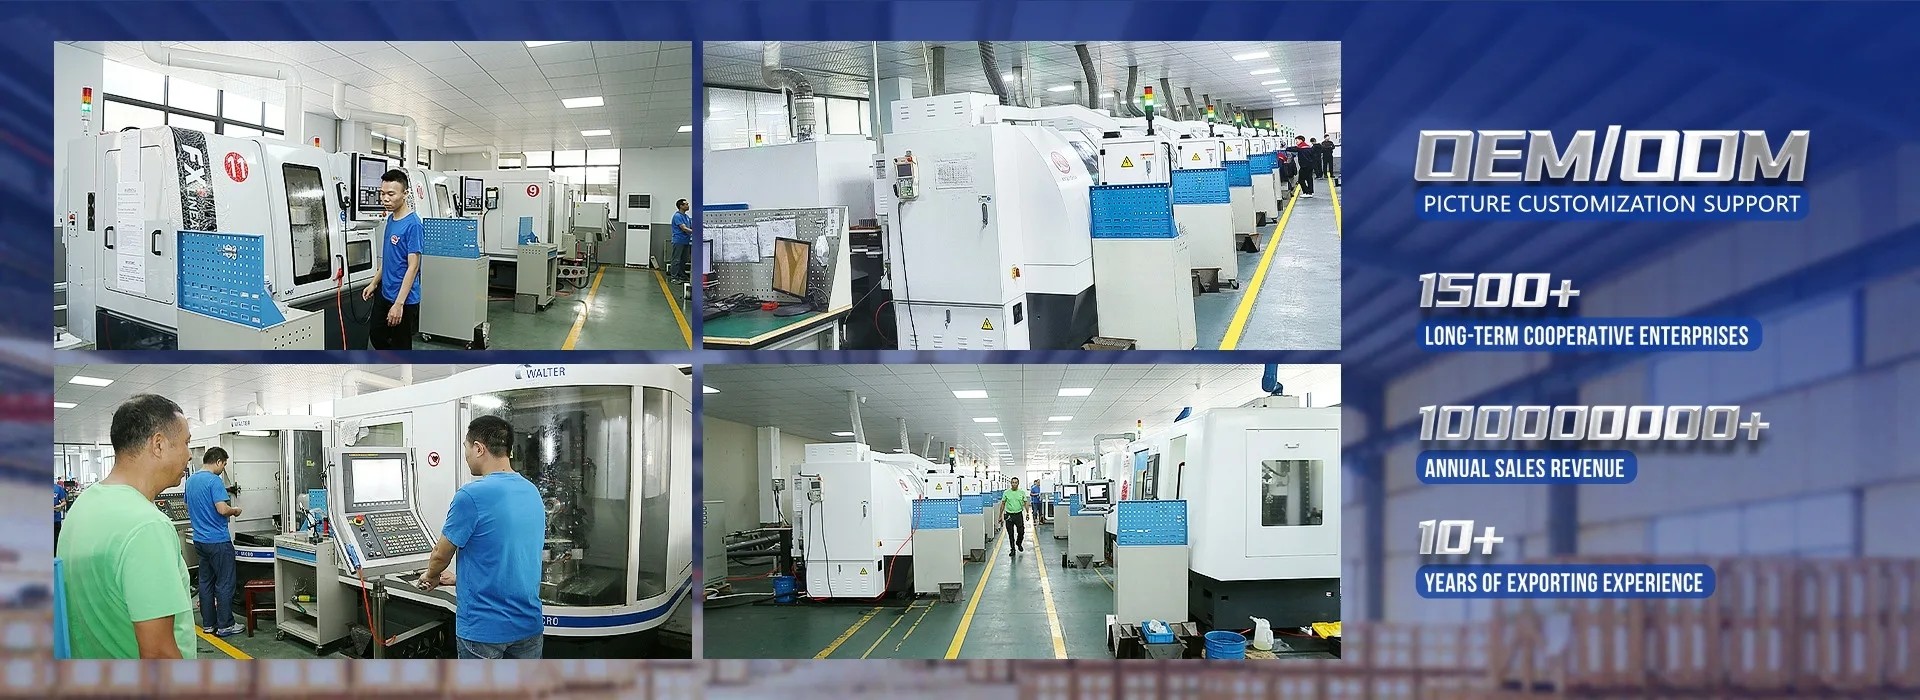
Supal (Changzhou) Precision Tools Co., Ltd.Od wielu lat zajmuje się projektowaniem, produkcją i sprzedażą narzędzi z twardych węglików, z całkowitą inwestycją ponad 10 milionów, i składa się z grupy doświadczonych pracowników.Jako profesjonalny producent narzędzi, stał się jednym z członków zarządu Stowarzyszenia Narzędzi Changzhou Xiaxiashu.ANCA z Australii i pięcioościowe maszyny do szlifowania NCPonadto przedsiębiorstwo jest wyposażone w automatyczny detektor obcinkowy firmy ZOLLER oraz ultra ...
Ucz się więcej

0

Rok założenia:

0

Milion+
Pracownicy

0

Milion+
Coroczne wyprzedaże:
Chiny Supal (Changzhou) Precision Tools Co.,Ltd Wysoka jakość
Pieczęć zaufania, kontrola kredytu, RoSH i ocena zdolności dostawcy. Firma ma ściśle kontrolowany system jakości i profesjonalne laboratorium badawcze.
Chiny Supal (Changzhou) Precision Tools Co.,Ltd Rozwój
Wewnętrzny profesjonalny zespół projektowy i warsztat zaawansowanych maszyn. Możemy współpracować, aby opracować produkty, których potrzebujesz.
Chiny Supal (Changzhou) Precision Tools Co.,Ltd Produkcja
Zaawansowane automatyczne maszyny, ściśle kontrolowane procesem. Możemy wyprodukować wszystkie terminale elektryczne, które nie są wymagane.
Chiny Supal (Changzhou) Precision Tools Co.,Ltd 100% SERWIS
Opakowania masowe i małe na zamówienie, FOB, CIF, DDU i DDP. Pozwól nam pomóc Ci znaleźć najlepsze rozwiązanie dla wszystkich twoich problemów.

Jakość Frezowanie narzędzi z węglika spiekanego & frezy walcowo-czołowe Producent

Znajdź produkty, które lepiej spełniają Twoje wymagania.
Sprawy i wiadomości
Najnowsze gorące punkty.
Nierównomierne zużycie rowków we frezach węglikowych: przyczyny i rozwiązywanie problemów
Nierówne zużycie rowka frezów z węglików spiekanych: przyczyny i rozwiązywanie problemów Frez palcowy z węglików spiekanych może wykazywać akceptowalną wydajność na jednym rowku i nieprawidłowe zużycie, odpryski lub narosty na krawędzi innego. Za ten nierówny stan często obwinia się nierówną jakość węglika, ale wzór często wskazuje na bicie, trzymanie narzędzia, mocowanie robocze, zazębienie lub wibracje. Gdy jedno rowek przenosi większe obciążenie skrawaniem, narzędzie może wcześnie ulec uszkodzeniu, nawet jeśli zaprogramowana prędkość i posuw wydają się rozsądne. Dla mechaników CNC, inżynierów procesów i inżynierów ds. zakupów nierównomierne zużycie rowka wiórowego jest cennym dowodem diagnostycznym. Lokalizacja i rozkład zużycia mogą pomóc w odróżnieniu problemu z narzędziem od problemu z ustawieniem. Dlatego też w ramach praktycznego badania należy zbadać łącznie używane narzędzie, oprawkę, maszynę, przedmiot obrabiany, ścieżkę narzędzia, kształt wióra i parametry skrawania, a nie wymieniać narzędzie bez zidentyfikowania braku równowagi obciążenia. W tym przewodniku wyjaśniono typowe przyczyny nierównomiernego zużycia rowków frezów walcowo-czołowych z węglików spiekanych, jak interpretować wzór zużycia i jak ustalić kontrolowaną sekwencję korekcji. Jak wygląda nierówne zużycie fletu Nierównomierne zużycie oznacza, że ​​rowki nie dzielą pracy skrawania w w miarę spójny sposób. Różnica może wyglądać następująco: Jeden flet z zauważalnie większym zużyciem powierzchni bocznej Odpryski skoncentrowane na jednej krawędzi skrawającej Materiał zabudowany przymocowany tylko do jednego fletu Różne zaokrąglenia krawędzi od fletu do fletu Na jednym ostrzu błyszcząca przetarcia, na drugim normalne ślady cięcia Ślady drgań odpowiadające przeciążonej części narzędzia Nagła utrata wykończenia lub stabilności wymiarowej po krótkim cyklu cięcia Narzędzie należy sprawdzać przy stałym oświetleniu i, jeśli to możliwe, pod powiększeniem. Zanotuj, który rowek wykazuje największe zużycie, gdzie wzdłuż osiowej długości skrawania zaczyna się uszkodzenie i czy wzór powtarza się na wielu narzędziach tego samego ustawienia. Pojedyncze uszkodzenie rowka nie świadczy o tym, że narzędzie zostało wykonane nieprawidłowo. Jeżeli w tym samym uchwycie lub maszynie wielokrotnie występuje awaria tej samej pozycji rowka, ustawienie staje się bardziej prawdopodobnym źródłem nierównomiernego obciążenia. Najczęstsza przyczyna: bicie Dlaczego bicie przeciąża jeden flet Bicie promieniowe zapobiega usuwaniu przez wszystkie rowki wiórów o tej samej grubości. Jeden flet może uderzać mocniej, podczas gdy inny flet usuwa niewielką ilość materiału lub ociera się. Przeciążony rowek jest poddawany większym naprężeniom mechanicznym i termicznym, co może prowadzić do przyspieszonego zużycia, wykruszania się lub narostu na krawędzi. Bicie może wystąpić na wrzecionie, uchwycie, tulei zaciskowej, nakrętce tulei zaciskowej, chwycie narzędzia lub powierzchni osadzenia narzędzia. Można go także wzmocnić długą projekcją lub uszkodzonym interfejsem. Mała wartość bicia może stanowić znaczny procent narzędzia o małej średnicy, więc akceptowalny stan zależy od średnicy narzędzia i zastosowania, a nie od jednej uniwersalnej liczby. Praktyczna kontrola bicia Użyj normalnej, zatwierdzonej metody pomiaru i sprawdź, jak najbliżej krawędzi skrawającej. Przed pomiarem oczyść chwyt narzędzia, tuleję zaciskową, nakrętkę, stożek uchwytu i złącze wrzeciona. Sprawdź, czy narzędzie jest prawidłowo osadzone i czy elementy uchwytu nie są zużyte ani uszkodzone. Nie należy stosować redukcji parametrów jako substytutu korekcji niedopuszczalnego bicia. Obniżenie posuwu może zmniejszyć średnie obciążenie, pozostawiając ten sam rowek przeciążony przy każdym obrocie. Problemy z trzymaniem i osadzaniem narzędzi Zanieczyszczenia i uszkodzenia powierzchni stykowych Mały wiór, zadzior, film olejowy lub cząstka pomiędzy chwytem a tuleją zaciskową mogą przechylić narzędzie. Rezultatem może być nierówne obciążenie rowka, nawet jeśli uchwyt wydaje się ciasny. Podczas każdej wymiany narzędzia należy sprawdzać powierzchnie stykowe i postępować zgodnie z procedurą czyszczenia. Stan tulei i uchwytu Zużyta tuleja zaciskowa może nierównomiernie chwytać lub nie wspierać koncentrycznie trzpienia. Uszkodzona nakrętka zaciskowa, stożek uchwytu lub interfejs wrzeciona mogą powodować podobne objawy. Jeśli kilka narzędzi wykazuje ten sam wzór zużycia z jednym rowkiem, przetestuj oprawkę za pomocą znanego, stabilnego narzędzia lub przenieś operację na zweryfikowaną oprawkę przed zmianą geometrii narzędzia. Nadmierna projekcja Ugięcie narzędzia zwiększa się wraz z występem. Długie narzędzie może odsunąć się od zaprogramowanej ścieżki, szczególnie podczas ciężkiego cięcia promieniowego lub gdy przedmiot obrabiany nie jest sztywny. Ugięcie zmienia rzeczywiste zaangażowanie i może spowodować, że jeden obszar narzędzia będzie pracował ciężej, niż oczekiwano. W przypadku głębokich funkcji użyj najkrótszego praktycznego narzędzia. Jeśli nie da się uniknąć większego zasięgu, należy wziąć pod uwagę równowagę geometrii i sztywności oferowaną przezFrezy trzpieniowe z długą szyjkąi sprawdź całą konfigurację, zamiast zakładać, że dłuższe narzędzie może wykorzystywać te same parametry skrawania, co krótkie narzędzie. Ścieżka narzędzia i efekty zaangażowania Nierówne zaangażowanie na zakrętach Narzędzie może podlegać większemu obciążeniu w narożnikach, wejściach i wyjściach lub przy zmianach promieniowego sprzężenia. Jeśli ten sam rowek wielokrotnie napotyka sekcję o największym obciążeniu ze względu na bicie lub orientację ścieżki narzędzia, wzór zużycia może stać się silnie asymetryczny. Przejrzyj zaprogramowane połączenie promieniowe i osiowe w miejscu, w którym zaczyna się uszkodzenie. Porównaj symulację CAM z rzeczywistym przedmiotem obrabianym, w tym zmiennością półfabrykatu, naskórkiem odlewu, otworami poprzecznymi i obszarami przerwanymi. Cięcie i rowkowanie na całej szerokości Zaangażowanie na całej szerokości zwiększa obciążenie promieniowe i pozostawia mniej miejsca na ucieczkę wiórów. Jeśli występuje bicie, przeciążony rowek może również napotkać upakowane wióry, zwiększając ryzyko odprysków i nagrzania. Jeśli funkcja na to pozwala, zastosuj strategię mniejszego promieniowego zaangażowania lub oddzielne przejścia obróbki zgrubnej i wykańczającej. Wstrząsy wejściowe i wyjściowe Nagłe zanurzenie, niepodparte wyjście lub nagła zmiana zaangażowania mogą spowodować uderzenie, które uszkodzi jeden róg lub rowek. Jeśli narzędzie ulegnie awarii natychmiast po wejściu, przed zmianą powłoki sprawdź metodę wprowadzenia, podparcie przedmiotu obrabianego i rzeczywisty stan wejścia. Mocowanie i sztywność maszyny Nierównomierne zużycie rowka może powstać na zewnątrz narzędzia. Poruszający się przedmiot obrabiany, uginająca się cienka ściana lub uchwyt z nieodpowiednim podparciem zmieniają obciążenie skrawania podczas przejścia. Narzędzie może wówczas naprzemiennie trzeć i uderzać, powodując nieregularny wzór zużycia. Sprawdź kontakt uchwytu, siłę mocowania, podparcie pod cienkimi sekcjami i sztywność łańcucha obrabiarka-przedmiot obrabiany. Słuchaj zmian w dźwięku, gdy nóż porusza się po różnych obszarach części. Jeśli zużycie koncentruje się w miejscu, w którym część jest najmniej podparta, podstawową korektą może być trzymanie materiału. Chatter może również przeciążać wybrane krawędzie. Geometria o zmiennym skoku lub inna geometria kontrolująca wibracje może być pomocna w odpowiednim zastosowaniu, ale nie może zastąpić korekty nadmiernego wysięgu, bicia, słabego mocowania lub niestabilnej ścieżki narzędzia. Zagadnienia dotyczące materiału, geometrii i powłoki Dopasuj narzędzie do obrabianego przedmiotu Geometria narzędzia powinna odzwierciedlać zdolność materiału do tworzenia wiórów, twardość, tendencję do przylegania i poziom przerw. Ostra krawędź może ułatwić czyste ścinanie w materiale podatnym na przyleganie, natomiast twardsze przygotowanie krawędzi może być bardziej odpowiednie, gdy dominuje zużycie udarowe lub ścierne. PorównującNarzędzia do frezowania węglików spiekanych, przejrzyj liczbę rowków, spiralę, wytrzymałość rdzenia, przygotowanie krawędzi, podłoże i powłokę jako jeden system. Jest mało prawdopodobne, aby sama zmiana powłoki naprawiła przeciążenie jednego rowka spowodowane biciem. Powłoka podlega mechanizmowi awarii Wybór powłoki powinien opierać się na dominującym trybie zniszczenia. Przyczepność, zużycie termiczne i ścieranie wymagają różnych strategii. Jeśli na jednym rowku widać zespawany materiał, a na innym tarcie, najpierw sprawdź nierówne obciążenie i powstawanie wiórów. Jeśli powłoka łuszczy się równomiernie na połączonych krawędziach, na większą uwagę mogą zasługiwać warunki termiczne lub przyczepność. Wszelkie zalecenia dotyczące powłoki lub geometrii należy traktować jako punkt odniesienia i weryfikować je w odniesieniu do rzeczywistej maszyny, oprawki, uchwytu roboczego, metody podawania chłodziwa i gatunku materiału. Kiedy niestandardowa geometria jest uzasadniona Standardowe narzędzie może nie zapewniać wymaganej kombinacji zasięgu, przestrzeni rowka, wytrzymałości narożników i stabilności połączenia w przypadku złożonej funkcji. W takiej sytuacjiNiestandardowe narzędzia frezarskiemożna ocenić w oparciu o rzeczywistą cechę i wzór awarii. Opcja niestandardowa powinna nadal zostać sprawdzona w kontrolowanych próbach; dostosowywanie nie eliminuje konieczności korygowania niestabilności konfiguracji. Kontrolowana sekwencja rozwiązywania problemów W przypadku stwierdzenia nierównomiernego zużycia rowka należy zastosować się do poniższej kolejności, aby uniknąć jednoczesnej zmiany kilku zmiennych: Zachowaj i sprawdź uszkodzone narzędzie. Sfotografuj każdy rowek i zapisz czas cięcia lub liczbę części. Określ, czy uszkodzenie jest zużyciem, odpryskami, narostem na krawędzi, przetarciem, czy może kombinacją tych uszkodzeń. Oczyść i sprawdź chwyt, tuleję zaciskową, oprawkę, złącze wrzeciona i powierzchnie osadzania narzędzia. Zmierz bicie, stosując normalną procedurę, tak blisko krawędzi skrawającej, jak to możliwe. Sprawdź występ narzędzia, zazębienie osiowe, zazębienie promieniowe oraz rzeczywiste warunki wejścia i wyjścia. Potwierdź trzymanie i podparcie, zwłaszcza w pobliżu cienkich ścian, szczelin lub przerwanych obszarów. Sprawdź kształt wióra i jego ewakuację. Poszukaj spakowanych wiórów lub śladów ponownego cięcia. Sprawdź gatunek materiału, geometrię narzędzia, powłokę, metodę podawania chłodziwa i parametry skrawania. Zmień jedną główną zmienną i przeprowadź kontrolowane porównanie. Zapisz wynik przed wprowadzeniem kolejnej zmiany. Parametry skrawania należy traktować jako punkt wyjścia dla konkretnego narzędzia i zastosowania. Muszą zostać sprawdzone pod kątem konkretnej maszyny, uchwytu, uchwytu roboczego i gatunku materiału, zanim zostaną przyjęte jako proces standardowy. Rozwiązywanie problemów według wzoru zużycia Jeden flet ma silne ślady użytkowania na boku Najpierw sprawdź bicie, osadzenie narzędzia, stan tulei zaciskowej i zazębienie ścieżki narzędzia. Upewnij się, że przeciążony rowek nie wchodzi wielokrotnie w narożnik lub obszar z ubitymi wiórami. Jeden flet jest wyszczerbiony, pozostałe wyglądają na nadające się do użytku Sprawdź warunki uderzenia, przerwany materiał, strategię wejścia i wyjścia, bicie oprawki i ruch przedmiotu obrabianego. Jeśli awaria powtarza się w tej samej lokalizacji ścieżki, przejrzyj to przejście w programie CAM i na części. Jeden flet ma zabudowany brzeg Zwróć uwagę na tarcie, nierówną grubość wiórów, niewystarczające odprowadzanie wiórów i problemy z przyczepnością specyficzną dla materiału. Sprawdź ostrość krawędzi, wypolerowanie rowka, smarowanie i powłokę dopiero po sprawdzeniu nierównego obciążenia. Wszystkie flety noszą ślady użytkowania, ale jeden jest znacznie gorszy Ten wzór może wskazywać ogólne obciążenie procesu w połączeniu z biciem lub ugięciem. Przejrzyj ogólne dane dotyczące zaangażowania i skrawania, a następnie sprawdź, dlaczego jeden rowek przenosi dodatkowe obciążenie. Zużycie różni się w zależności od części Niespójne mocowanie, wahania zapasów, stan materiału, upakowanie wiórów lub zmiany termiczne mogą powodować zmianę stabilności procesu. Zanotuj lokalizację części i czas pojawienia się różnicy w zużyciu. Typowe błędy, których należy unikać Wymiana narzędzia bez sprawdzania uchwytu Nowe narzędzie w tym samym niestabilnym uchwycie może odtworzyć ten sam wzór zużycia. Zanim stwierdzisz, że narzędzie jest wadliwe, sprawdź cały łańcuch mocowania narzędzia. Zmniejszenie posuwu jako jedyna korekta Zmniejszenie posuwu może tymczasowo ukryć objaw, pozostawiając bicie, tarcie lub uderzenie bez zmian. Może również powodować niewystarczającą grubość wiórów i większą ilość ciepła. Obwinianie powłoki przed sprawdzeniem obciążenia Powłoka nie może sprawić, że wszystkie rowki będą dzielić obciążenie, gdy występuje bicie lub ugięcie. Przed wyborem innej powłoki należy zdiagnozować przyczynę mechaniczną. Ignorowanie pozycji rowka uszkodzonego narzędzia Przydatnym dowodem jest położenie uszkodzonego fletu. Zapisuj to konsekwentnie, zamiast wyrzucać narzędzie bez kontroli. Jednoczesna zmiana prędkości, posuwu, geometrii i chłodziwa Wiele jednoczesnych zmian utrudnia interpretację wyniku. Korzystaj z kontrolowanych prób i dokumentuj jedną podstawową zmianę na raz. Często zadawane pytania Co powoduje, że jeden rowek frezu palcowego z węglików spiekanych zużywa się szybciej niż pozostałe? Typowe przyczyny obejmują bicie promieniowe, złe osadzenie narzędzia, zużytą tuleję zaciskową, nadmierny występ, nierówne sprzężenie, ruch przedmiotu obrabianego, gromadzenie się wiórów i wibracje. Przed założeniem, że występuje defekt węglika lub powłoki, należy sprawdzić całą konfigurację. Czy bicie frezu walcowo-czołowego może powodować odpryski? Tak. Bicie może spowodować przeciążenie jednego fletu i spowodować tarcie innego fletu. Przeciążona krawędź może szybko wykruszać się lub zużywać, zwłaszcza podczas przerywanej obróbki, obróbki na całej szerokości lub operacji z ograniczonym odprowadzaniem wiórów. Czy powinienem zmienić powłokę, gdy na jednym z rowków widać narost? Nie natychmiast. Najpierw sprawdź bicie, ostrość krawędzi, grubość wióra, odprowadzanie wiórów, smarowanie i kompatybilność materiału. Zmiana powłoki może pomóc tylko wtedy, gdy dominujący mechanizm uszkodzenia odpowiada zamierzonej funkcji powłoki. Jak mogę stwierdzić, czy nierówne zużycie jest spowodowane drganiami, czy biciem? Bicie często powoduje stałą nierównowagę pomiędzy rowkami, podczas gdy drgania mają tendencję do tworzenia powtarzających się śladów wibracji i mogą zmieniać się w zależności od włączenia lub prędkości wrzeciona. Obydwa mogą współistnieć, dlatego należy sprawdzić narzędzie, oprawkę, wspornik przedmiotu obrabianego i wzór powierzchni razem. Jakie informacje powinienem podać, prosząc o zalecenie dotyczące rozwiązywania problemów? Podaj gatunek materiału, średnicę narzędzia i liczbę rowków, zasięg i wysięg, typ oprawki, zmierzone bicie, jeśli jest dostępne, parametry skrawania, sprzężenie promieniowe i osiowe, metodę podawania chłodziwa, szczegóły mocowania, liczbę części i wyraźne zdjęcia każdego rowka. Wniosek Nierównomierne zużycie rowka to nie tylko problem związany z wymianą narzędzia; stanowi to dowód na to, że obciążenie tnące nie jest rozkładane zgodnie z przeznaczeniem. Przed zmianą gatunku narzędzia lub powłoki należy wziąć pod uwagę bicie, osadzenie narzędzia, stan oprawki, nadmierny występ, ruch przedmiotu obrabianego, zmiany zazębienia, gromadzenie się wiórów i wibracje. Niezawodna sekwencja korekcyjna chroni uszkodzone narzędzie, identyfikuje wzór zużycia, weryfikuje łańcuch mocowania narzędzia, sprawdza zaangażowanie i trzymanie narzędzia oraz zmienia jedną główną zmienną na raz. Jeśli proces nadal wymaga szczególnej równowagi między zasięgiem, przestrzenią na wióry i wytrzymałością krawędzi, narzędzie zaprojektowane specjalnie do tego celu można ocenić po ustabilizowaniu się podstawowej konfiguracji. Jeśli Twój frez węglikowy wykazuje zużycie jednoostrzowe, powtarzające się odpryski, narost na krawędzi lub niestabilną trwałość narzędzia,Skontaktuj się z Supalemz gatunkiem materiału, aktualnym narzędziem, szczegółami uchwytu i wysięgu, danymi skrawania i zdjęciami każdego rowka. Informacje te pomagają określić praktyczny punkt początkowy geometrii i procesu do walidacji na maszynie.
2026

10/13

Corner Radius vs Square End Mills for Interrupted Shoulder Milling
Corner Radius vs Square End Mills for Interrupted Shoulder Milling Interrupted shoulder milling is one of the operations where end mill geometry has a direct effect on edge stability. When the cutter repeatedly enters and exits the workpiece, passes across gaps, or encounters uneven stock, each tooth experiences a changing load instead of a smooth continuous cut. A square end mill can produce a sharp 90-degree shoulder, while a corner radius end mill can distribute load around the tool corner and reduce local stress. Choosing between them requires more than looking at the drawing requirement. For CNC machinists, process engineers, and purchasing engineers, the correct decision depends on the balance between required corner definition, interruption severity, tool rigidity, material, engagement, and finishing strategy. This guide compares square and corner-radius geometries for interrupted shoulder milling and explains how to diagnose edge chipping, chatter, poor finish, and unstable tool life. What Makes Interrupted Shoulder Milling Difficult? In a continuous side-milling cut, the cutting edge enters the workpiece and remains engaged in a relatively predictable way. In an interrupted shoulder operation, the edge may encounter a slot, a cross-hole, a casting irregularity, a forged surface, a previous pocket, or an open boundary. Each interruption changes the force and can create impact at entry or exit. The highest-risk conditions usually include: Repeated entry and exit at the same corner of the tool Full radial engagement at a 90-degree shoulder Thin walls or weak workholding that move during the cut Long tool overhang or poor holder runout Abrasive scale, cast skin, or hard inclusions Excessive feed or engagement at the interruption point A sharp square corner exposed to repeated impact A tool can therefore fail even when the average cutting load appears acceptable. The peak impact load, not only the average spindle load, may determine whether the edge survives. Square End Mills: Strengths and Limits A Square End Mill is the natural choice when the part requires a sharp internal shoulder or a flat-bottomed slot. Its geometry can produce a defined 90-degree corner without leaving a programmed radius at the bottom of the wall. When a Square End Mill Is Appropriate Square end mills are often considered when: The finished feature requires a sharp shoulder The toolpath uses stable, continuous engagement The workpiece and fixture are rigid The interruption is limited or can be approached with a controlled entry A separate finishing pass can protect the final corner quality The tool diameter and reach provide sufficient core strength A square tool can perform well in interrupted milling when the edge is properly supported and the engagement is controlled. It should not be rejected simply because the cut is interrupted; the severity and location of the interruption matter. Where Square Corners Become Vulnerable The tool corner is a stress concentration. During an interrupted cut, the corner may take a sudden impact as it enters the material. If the tool is also deflecting, the corner can receive more load than the other flutes. Typical results include corner chipping, a small radius appearing on the part after wear, chatter marks, or an abrupt change in surface finish. A sharp corner can also be sensitive to hard spots, scale, and thin-wall movement. If the failure is concentrated at the corner while the side cutting edges remain relatively intact, geometry and engagement should be reviewed before changing coating alone. Corner Radius End Mills: Strengths and Limits A Corner Radius End Mill includes a controlled radius between the end face and peripheral cutting edge. The radius removes the most fragile sharp corner and distributes cutting load over a larger region of the tool tip. When a Corner Radius Is Advantageous A corner-radius tool is often considered when: The cut includes repeated entry and exit The operation encounters an interrupted or uneven surface Edge chipping is concentrated at a square corner The part drawing permits a small internal radius The operation uses higher engagement or heavier roughing The process needs additional corner strength and more stable tool life The radius does not eliminate vibration or poor setup conditions, but it can reduce the severity of a localized corner impact. It may also improve the tool’s tolerance of intermittent engagement when compared with an otherwise similar sharp-corner tool. The Geometric Trade-Off The main limitation is straightforward: a corner radius leaves a radius on the finished shoulder. If the part requires a sharp 90-degree internal corner, the radius may need to be removed by a secondary operation or replaced by a square finishing tool. A corner radius can also change the effective engagement and contact area. It should be evaluated together with axial depth, radial engagement, tool diameter, and the required surface finish rather than selected based on radius size alone. How to Choose Between the Two Geometries Start With the Drawing Requirement First identify whether a sharp internal corner is functionally required or simply shown as a nominal feature. If a small radius is acceptable, a corner-radius tool may provide a more robust roughing or semi-finishing process. If a sharp corner is essential, use a square tool where practical or plan a roughing-and-finishing sequence that controls the load on the final square edge. Identify the Interruption Type Not all interruptions have the same effect. A predictable open boundary may be easier to manage than a hard casting skin or an irregular forged surface. Cross-holes and slots can create repeated impact at a known location, while uneven stock can make the load unpredictable. Record where the first damage occurs. If chipping starts at every entry point, the issue may be impact or lead-in strategy. If it appears only at a particular section of the workpiece, inspect material condition and support at that location. Match the Tool to the Operation For roughing and semi-finishing, the added corner support of a radius can be valuable when the operation is interrupted. For finishing, a square tool may be preferred if the corner specification requires it and the setup can maintain stable engagement. A practical process may use a corner-radius tool for stock removal, followed by a square end mill for the final shoulder. The two tools should not automatically use identical cutting conditions; the finishing tool may require a different engagement and a more controlled pass. Geometry, Edge Preparation, and Coating Edge Preparation A completely sharp edge may reduce cutting force in some materials, but it can be vulnerable to impact. A lightly reinforced edge may provide better stability in interrupted cuts, although excessive edge honing can increase rubbing and heat. The appropriate edge preparation depends on the workpiece, interruption severity, tool diameter, and operation. When comparing tools, request information about edge preparation rather than evaluating only flute count or coating name. Two tools with similar descriptions may behave differently if their edge preparation and carbide substrate differ. Helix and Flute Configuration Helix and flute count influence force direction, chip evacuation, and the number of teeth sharing the load. A higher flute count may support feed capacity in a light radial finishing pass, while a roughing or interrupted operation may need more chip space and a stronger core. The right balance depends on the material and engagement. A tool with insufficient flute space may recut chips, while a tool with a very thin core may lack impact resistance. Select from the broader Carbide Milling Tools range based on the actual operation rather than relying on the end mill shape alone. Coating Coating should follow the dominant failure mechanism. A coating may help manage heat, adhesion, or abrasive wear, but it cannot compensate for excessive tool deflection, a sharp corner overloaded by impact, or an unstable fixture. If the tool chips at entry, check geometry and rigidity before assuming that a coating change is the primary solution. Any coating recommendation should be validated with the specific material, tool geometry, coolant strategy, and cutting conditions. Treat supplier data as a starting reference and confirm the result on the actual machine. Parameter Strategy for Interrupted Shoulder Milling Cutting data should be treated as a starting reference for the exact diameter, flute count, coating, material grade, tool overhang, and machine setup. Do not transfer a value from a continuous side-milling operation directly to an interrupted shoulder cut without validation. Control the Peak Load at Entry Entry conditions can create the highest impact. Where the geometry allows, use a ramp, arc, or controlled lead-in instead of an abrupt radial plunge. This reduces the sudden change from no load to full engagement. If a direct entry is unavoidable, review feed and radial engagement at the entry point. A controlled reduction in engagement or a separate approach pass may protect the edge better than reducing the entire program feed. Avoid Excessive Full-Width Engagement Full-width shoulder milling creates significant radial load. In an interrupted condition, the load can change sharply as the tool crosses the gap. If possible, use a reduced radial engagement strategy for roughing and leave a controlled allowance for finishing. The correct engagement depends on the tool, material, machine, and feature geometry. Validate changes with spindle load, sound, chip form, and edge inspection rather than assuming that a smaller engagement is always better. Adjust Speed and Feed One Variable at a Time If the tool chips, do not immediately reduce both speed and feed. First determine whether the damage is impact-related, vibration-related, or caused by rubbing. A feed reduction that is too large can create a thin chip and increase rubbing, while a speed change may affect heat and resonance differently. Change one parameter at a time and document the effect. Include the location of the failure, chip appearance, surface finish, and tool condition in the record. Diagnosing Common Failure Symptoms Corner Chipping on a Square End Mill Check interruption severity, tool entry, runout, edge preparation, and whether the square corner is taking the full impact. If the drawing permits it, compare a corner-radius tool in the roughing or semi-finishing stage. If a square corner is mandatory, reduce entry shock and ensure the finishing pass has consistent stock. Chatter on a Corner-Radius Tool A radius does not remove the need for rigidity. Check tool overhang, holder condition, workholding, spindle speed, axial depth, and radial engagement. Chatter may also result from a radius that creates an engagement pattern unsuitable for the current toolpath. Uneven Wear Between Flutes Uneven wear commonly points to runout, unequal flute loading, poor holder seating, or a workpiece that is moving. Inspect the shank, collet, holder, and setup before changing the tool geometry. Poor Shoulder Finish After Roughing A roughing tool with a damaged corner or built-up edge should not be used for a critical finishing pass. Clean the feature, use a sound finishing tool, and verify that the remaining allowance is consistent. If the finish still varies, inspect vibration and workholding. Short Tool Life at a Hard Spot If damage occurs only at a particular location, investigate material condition, scale, interrupted geometry, or inadequate support. A different corner geometry may help, but the toolpath and entry strategy should also be reviewed. Common Mistakes to Avoid Choosing a Square Tool Only Because the Part Has a 90-Degree Corner A square finishing tool may be correct for the final feature but unnecessarily vulnerable during heavy interrupted roughing. Separate stock removal from final corner generation when the process requires both robustness and a sharp corner. Assuming a Corner Radius Always Solves Chipping The radius can improve corner strength, but it does not fix excessive overhang, runout, unstable workholding, poor parameters, or a damaged holder. Reducing Feed Aggressively After Chipping A large feed reduction can cause rubbing and heat. Determine whether the first damage occurred at entry, during an interruption, or under continuous cutting before making broad changes. Ignoring Toolholding The geometry selected on paper cannot compensate for poor holder cleanliness, excessive runout, or unnecessary projection. Check the actual holder and machine setup. Mixing Roughing and Finishing Requirements One tool rarely provides the best combination of high interruption tolerance, high stock-removal capacity, sharp 90-degree finishing, and final surface quality. Define which pass is responsible for each requirement. FAQ Is a corner radius end mill stronger than a square end mill? The radius removes the sharpest corner stress concentration and can improve resistance to local chipping in some interrupted operations. The actual result still depends on material, edge preparation, tool diameter, engagement, rigidity, and parameters. Should I use a corner radius for every interrupted shoulder cut? No. If a sharp 90-degree corner is required, a square end mill may still be necessary for finishing. A corner-radius tool can be considered for roughing or semi-finishing when the part permits a radius or a secondary finishing operation. Why does my square end mill chip only at the entry point? The entry may create an impact or engagement spike. Check lead-in strategy, radial engagement, feed at entry, runout, workpiece support, and the condition of the material surface at the entry location. Can changing the coating stop corner chipping? Only when the dominant failure involves heat, adhesion, or wear that the new coating is suited to control. Coating cannot correct an overloaded corner, poor rigidity, abrupt entry, or excessive engagement. What information should I provide when requesting an end mill recommendation? Provide the material grade, shoulder and interruption geometry, required corner condition, tool diameter and reach, machine and holder details, current parameters, coolant method, tool wear pattern, and photographs of the damaged edge or finished shoulder. Conclusion The choice between a corner-radius and square end mill for interrupted shoulder milling should begin with the part requirement, then consider interruption severity, edge strength, tool rigidity, engagement, and finishing strategy. A square end mill provides a sharp corner but concentrates stress at the tool tip. A corner-radius end mill distributes load more gradually and may reduce local chipping when a radius is acceptable. For demanding operations, a two-stage process can balance both objectives: use a robust geometry for interrupted roughing or semi-finishing, then use a square tool for the final shoulder when the drawing requires a sharp corner. Build parameters from the supplier’s starting range, change one variable at a time, and validate the complete process on the actual machine and workholding. If your shoulder milling process shows corner chipping, chatter, poor finish, or inconsistent tool life, Contact Supal with the material grade, interruption geometry, current tool, tool overhang, parameters, and photos of the failure. This information helps identify a practical geometry and process starting point for on-machine validation.

2026

10/06

How to Choose Carbide End Mills for Copper and Brass Machining
How to Choose Carbide End Mills for Copper and Brass Machining Copper, brass, bronze, and other copper alloys are often described as easy-to-cut materials because they are softer than hardened steel. That description can be misleading. Copper alloys can create very different machining problems depending on their purity, temper, alloying elements, work-hardening behavior, and chip form. A tool that produces a clean result in free-machining brass may rub, smear, or generate built-up edge in a more adhesive copper grade. For CNC machinists, process engineers, and purchasing engineers, reliable copper alloy milling starts with matching the tool to the actual failure mechanism. Edge sharpness, flute space, chip evacuation, workholding, coolant, and parameter validation usually matter more than simply choosing the hardest or most expensive coating. This guide explains how to select carbide end mills for copper and brass machining while reducing adhesion, burrs, heat, and unstable tool life. Why Copper and Brass Need Material-Specific Tool Selection Copper alloys combine several characteristics that influence milling stability: Copper conducts heat efficiently, so heat can move into the workpiece instead of remaining concentrated at the tool edge. However, local rubbing can still raise edge temperature and cause adhesion. Pure or highly ductile copper can produce continuous, gummy chips that are difficult to evacuate. Brass and bronze grades vary widely. Some produce short chips, while others create longer chips or abrasive particles. A dull edge may rub and smear the surface rather than shear it cleanly. Thin walls, small features, and poor workholding can amplify deflection and burr formation. The result is that “copper” or “brass” is not enough information for final tool selection. The exact alloy or grade, hardness or temper condition, feature geometry, and finishing requirement should be confirmed before adopting a production tool. Common Failure Symptoms in Copper Alloy Milling Built-Up Edge and Material Adhesion Built-up edge appears when copper or another ductile alloy adheres to the cutting edge. The tool may look sharp at the beginning of the cut but gradually develops a welded mass that changes the effective edge geometry. This can cause poor surface finish, burrs, dimensional variation, and sudden edge damage when the built-up material breaks away. Adhesion is often promoted by rubbing, insufficient chip evacuation, a dull edge, excessive dwell, or a surface treatment that is not suited to the material. Changing to a harder coating without correcting rubbing may not solve the problem. Smearing and Poor Surface Finish A smeared surface usually indicates that the tool is not shearing the material cleanly. Possible causes include insufficient chip thickness, a dull or heavily honed edge, poor tool runout, unstable workholding, or a speed/feed combination that leaves the tool rubbing instead of cutting. Burrs at Entry and Exit Copper and brass can produce burrs when the cutting edge pushes material away at the exit. Burr formation is influenced by tool sharpness, radial engagement, feed direction, workpiece support, and the condition of the edge. A finishing pass may reduce burrs, but the root cause should still be addressed in the toolpath and tool selection. Chipped Edge or Unexpected Tool Failure Carbide edge chipping in copper alloy milling is not always caused by a material that is too hard. Interrupted cuts, loose workholding, excessive runout, thin-wall deflection, collisions, and trapped chips can generate impact loads that damage the edge. If chipping is concentrated on one flute, inspect runout and setup balance before changing the carbide grade. Chip Packing and Recutting Long copper chips can remain in a pocket, slot, or narrow cavity. Once recut, they create additional heat and load, increasing the chance of built-up edge and surface scratching. Tool geometry and air or coolant direction should be selected with chip travel in mind, especially in deep features. Flute Geometry and Edge Sharpness Choose Enough Chip Space for the Operation Copper and ductile brass grades may require generous flute space so chips can leave the cutting zone before they are recut. A low-flute-count tool can be useful when chip evacuation is the primary limitation, but the correct flute count also depends on rigidity, engagement, feed, finish, and feature geometry. For a deep pocket or slot, prioritize a toolpath and geometry that provide a clear chip path. For a light finishing pass, a different flute configuration may be preferred if it provides the required surface quality without creating excess rubbing. Favor a Clean, Sharp Cutting Edge A sharp edge generally helps shear copper and brass rather than push or smear them. Excessive edge rounding can increase rubbing and heat. However, sharpness must be balanced against the risk of edge damage in interrupted cuts, cast surfaces, abrasive inclusions, or unstable fixtures. The best edge preparation is application-dependent. A stable finishing cut may benefit from a very sharp edge, while a roughing operation with impact risk may require controlled edge reinforcement. Request the intended edge preparation when comparing tools rather than judging only by the product title. Consider Polished Flutes and Rake Surfaces A smooth flute and rake surface can reduce friction and help chips slide away from the cutting edge. This is particularly relevant when the material tends to adhere or when the tool is used in a narrow cavity with limited chip clearance. Polishing alone does not replace the need for suitable flute volume, coolant, or air blast, but it can support cleaner chip transport. Coating and Substrate Considerations Copper alloy applications do not always benefit from the same coating choices used for hardened steel. The dominant issue may be adhesion and friction rather than oxidation or high-temperature wear. In some applications, uncoated polished carbide is appropriate because the sharp, low-friction surface is more important than a hard coating layer. For abrasive copper alloys, bronze grades, or materials containing hard particles, a coating or substrate selected for wear resistance may be useful. The correct choice depends on the exact alloy and failure mode. Do not assume that a coating marketed for hardened steel will automatically improve copper machining, and do not assume that an uncoated tool is correct for every bronze or filled alloy. When comparing copper tools with End Mills for Aluminum, use the aluminum tool as a reference only, not as an automatic substitute. Both material groups can be adhesion-prone, but the exact chip form, edge condition, and surface requirement may differ. Parameter Strategy for Copper and Brass Milling Start With the Actual Tool and Alloy Cutting data should be treated as a starting reference, not a guaranteed setting. The appropriate speed, feed, radial engagement, and axial depth depend on tool diameter, flute count, stickout, machine rigidity, workholding, alloy grade, and coolant or air-blast conditions. Validate the starting range on the actual machine before making it a standard process. Avoid Rubbing and Dwell If the tool spends too much time sliding along the surface, adhesion and smearing become more likely. Check whether the toolpath includes dwell at corners, excessive radial engagement, or a feed value that is too low for the selected edge geometry. A modest, controlled chip load is usually preferable to a cut dominated by rubbing, but the exact value must be validated for the tool and material. Control Chip Evacuation Direct air or coolant so chips move away from the cutting zone rather than being pushed back into the pocket. If chips are long, review flute volume, toolpath engagement, and the conditions that determine chip formation. Increasing fluid pressure without correcting nozzle direction or chip path may produce little improvement. Change One Variable at a Time When troubleshooting built-up edge, burrs, or poor finish, change only one major variable at a time: tool geometry, coating, speed, feed, engagement, or chip evacuation. Document the result. This makes it possible to identify the actual improvement instead of attributing every change to the last tool purchased. Toolholding, Workholding, and Feature Stability Even a well-selected tool can fail when the setup is unstable. Check tool runout, holder cleanliness, clamping length, and the shortest practical tool projection. Thin copper components and unsupported walls can deflect under cutting pressure, leaving burrs or dimensional error that look like a tool problem. For holes and finishing operations, coordinate the milling process with Carbide Drills and Carbide Reamers. A poor pre-hole or unstable entry can reduce the performance of the finishing tool even when the reamer itself is suitable. A Practical Selection and Troubleshooting Sequence Confirm the exact copper, brass, bronze, or copper-alloy grade and condition. Identify the dominant failure: adhesion, burrs, poor finish, chip packing, chipping, or dimensional drift. Select flute count and chip space based on engagement and chip travel, not on flute count alone. Review edge sharpness, rake surface, flute polish, coating, and substrate together. Check runout, overhang, workholding, and thin-wall support. Establish a conservative starting process and validate it on the actual setup. Adjust one variable at a time and record chip form, finish, burr condition, load behavior, and tool wear. Common Mistakes to Avoid Treating All Copper Alloys as Pure Copper Brass, bronze, and specialized copper alloys can produce very different chips and wear mechanisms. A recommendation for one grade should not be transferred automatically to another. Choosing Coating Before Identifying the Failure Mode If adhesion is the primary issue, friction and edge sharpness may deserve attention before thermal coating performance. If abrasion is dominant, the solution may require a different substrate or wear-resistant coating. Diagnose first. Using a Dull Tool for a Finishing Operation A worn edge can rub, smear, and create burrs even when the tool still appears usable. Replace or recondition the tool based on the required surface and dimensional result, not only on visible fracture. Ignoring Chip Travel in Pockets and Slots Long chips that remain in the cavity will be recut. Review toolpath direction, flute space, air blast, coolant placement, and the ability of the machine to clear chips. Copying Parameters From Steel or Aluminum Without Validation Copper alloy behavior is not identical to steel or aluminum. Use supplier data as a starting reference and confirm the process on the actual machine, workholding, and material grade. FAQ What type of carbide end mill is commonly used for copper? A sharp, low-friction tool with suitable chip space is often considered for copper, but the correct flute count, edge preparation, coating, and substrate depend on the exact alloy and operation. Confirm the choice against the material grade and feature geometry. Why does copper create built-up edge on the tool? Built-up edge is commonly associated with adhesion, rubbing, heat concentration, poor chip evacuation, or an edge condition that is not suited to the material. Review sharpness, flute polish, toolpath engagement, and validated parameters before changing coating alone. Is an uncoated carbide end mill suitable for brass and copper alloys? It can be suitable in some applications where a sharp, polished, low-friction edge is the priority. Abrasive bronze or filled copper alloys may require a different wear strategy. The exact recommendation should be confirmed for the specific grade and failure mode. How can I reduce burrs when milling copper? Check tool sharpness, runout, exit engagement, workpiece support, radial engagement, and feed direction. A finishing pass may help, but burr reduction is usually more reliable when the edge and toolpath are stable from the beginning. What information should I provide when requesting a copper alloy tool recommendation? Provide the exact alloy and condition, tool diameter and flute count, feature geometry, tool overhang, machine and holder details, current parameters, coolant or air-blast method, chip form, and photographs of the finish or worn edge. Conclusion Choosing carbide end mills for copper and brass machining requires more than selecting a standard tool for a soft material. The best starting point is to identify the alloy, failure mode, chip behavior, and setup stability. Sharp and suitable geometry, sufficient chip space, controlled friction, reliable evacuation, and validated parameters work together to reduce built-up edge, burrs, smearing, chipping, and inconsistent tool life. If your copper or brass operation has adhesion, burr, chip evacuation, surface-finish, or tool-life problems, Contact Supal with the material grade, feature geometry, current tool, parameters, and failure photos. This information helps evaluate a practical tool and process starting point for on-machine validation.

2026

10/01